- Home
- Resources
- Prepare your parts
Five things that make your coating job go right
A short checklist for fabricators, and for anyone bringing in a part. Each one saves a phone call, a delay or a flaw in the finish.
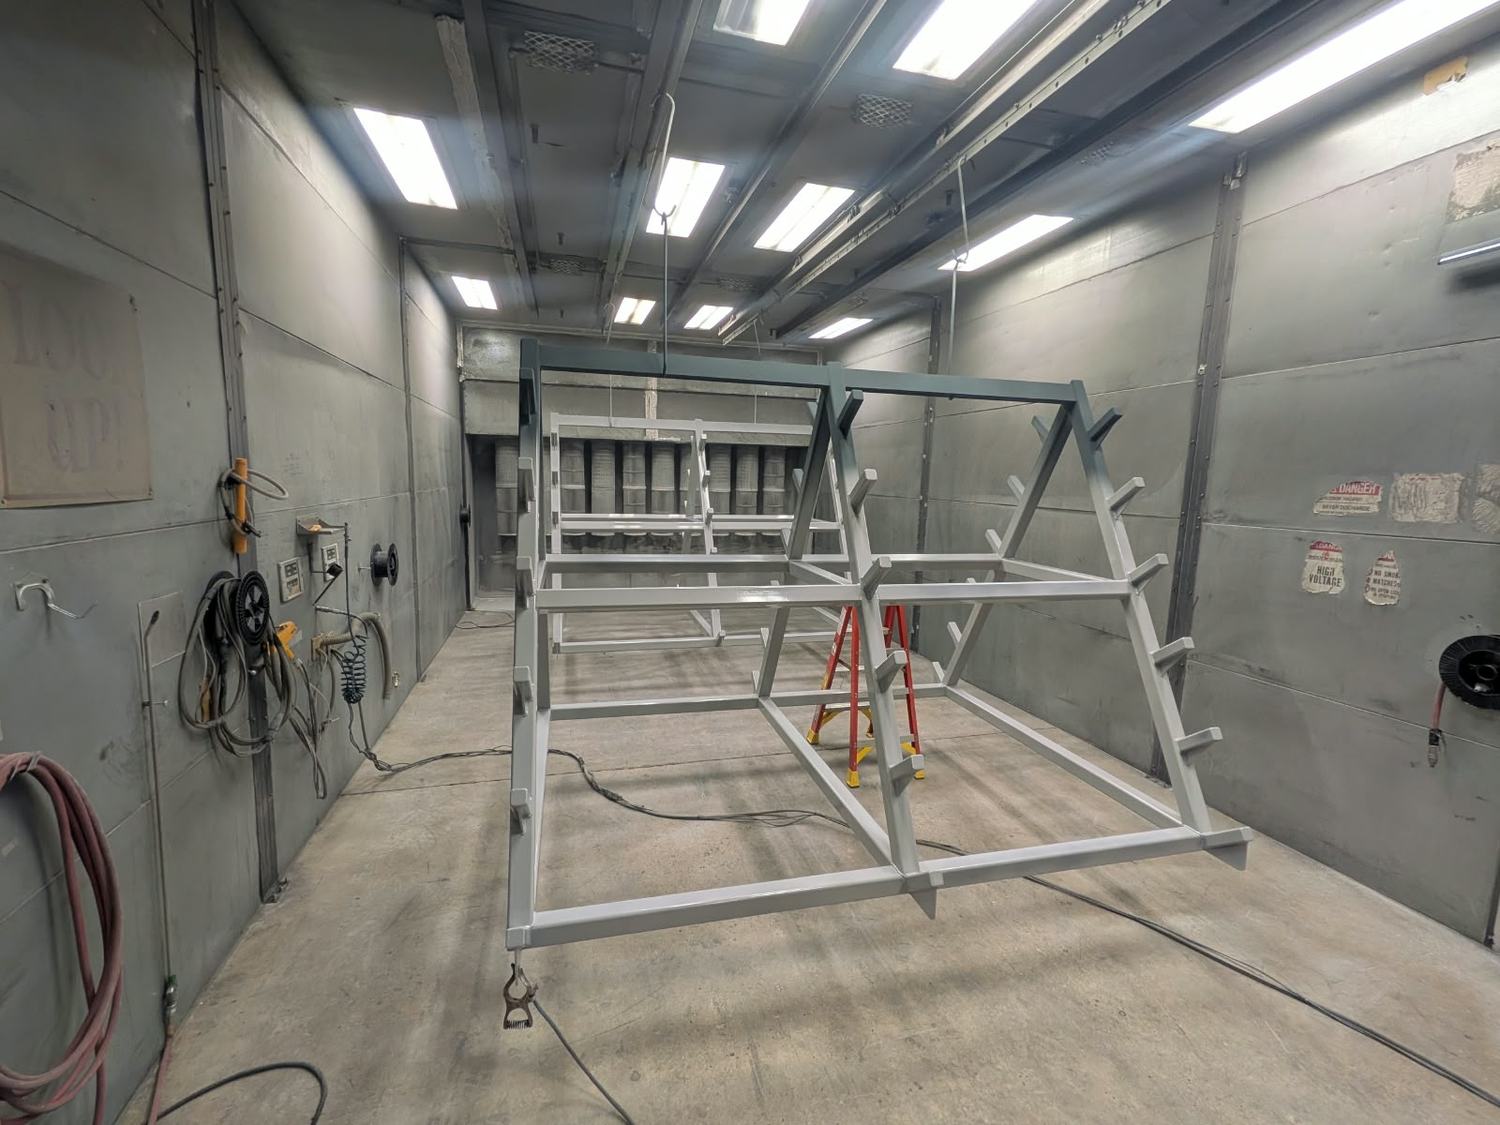
Clean it
Make sure the part is free of oil, grease and any other contaminants.
Remove what cannot be coated
Grease nipples, bearings, seals, silicones and rubber must come off. We reclaim and reuse our blast media, and one greasy part can ruin the whole batch, which costs thousands of dollars to replace.
Relieve sharp edges
Coatings do not bond well to a sharp 90 degree corner, and it becomes a failure point.
Check welds for porosity
Pinholes cannot be filled during the powder coating process, so welds need to be free of them.
Leave a hang point
We need a place to hang the part for coating. Hang points are touched up with an artist brush when the part is packaged.
Designing a part for powder
- Leave a hole or a tab we can hang the part from. Tell us where a hang mark is acceptable.
- Mark threads, bores and mating faces that must stay bare. We mask them with plugs and high-heat tape.
- Give trapped air and blast media a way out of closed sections.
- Check the part against our oven and blast room sizes before you weld it up.
What to send for a quote
- A drawing or photos
- Material and quantity
- Largest dimensions and weight
- Colour or coating spec
- The date you need it